Leading Technology Reputation First Leading Technology Reputation First
The technology leader in the credibility of the supremacy The technology leader in the credibility of the supremacy
Engaged in wear parts for twenty years Provide you with superior products and services Engaged in the manufacture of wear parts for twenty years, Provide you with superior products and value-added services
Why Choose Us ? -- Red Apple Casting Why Choose Us ?
We Have 20 Years Casting Experience.
We Will Supply You High Quality Hammers With Best Price.
We Have 20 Years Casting Experience.We Will Supply You High Quality Hammers With Best Price.
Mexico Client Agent of Latvian
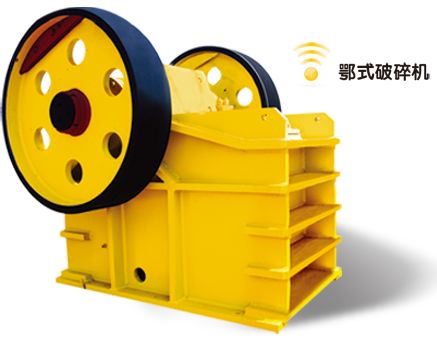
Learn how fixed and moving jaw plates crush material, how manganese steel work hardens, and what to check when selecting, ordering and maintaining replacement jaw plates.
Jaw plates, also called jaw dies or tooth plates, are the principal wear surfaces in a jaw crusher. A fixed plate and a moving plate form the crushing chamber. As the moving jaw approaches the fixed jaw, the feed is subjected to compression and associated splitting forces until it breaks.
Because the plates contact the feed directly, their condition affects crushing efficiency, product size and maintenance requirements. They should be treated as model-specific components, not as interchangeable plates selected by overall size alone.
High manganese steel is widely used for jaw plates because it can work harden under suitable impact and compressive loading while retaining a tough interior. The amount of work hardening depends on the actual duty; it is not a fixed hardness increase for every installation.
Material examples include ZGMn13, chromium-alloyed manganese grades such as ZGMn13Cr2, and higher-manganese grades such as Mn18 and Mn18Cr2. A higher manganese content does not automatically make a plate the best choice. Feed hardness, abrasiveness, particle size, crusher size and loading all need to be considered.
Casting quality, the specified heat treatment and dimensional control are important to performance. The required process should be matched to the selected alloy, plate thickness and approved drawing.
When ordering, identify the fixed or moving position, tooth profile, part number, mounting arrangement, bolt holes and drawing revision. Confirm the material grade and agreed inspection requirements before production.
Zhangjiakou Red Apple Machinery Equipment Manufacturing Co., Ltd., trading as Red Apple Casting, supplies wear-resistant castings for mining, cement and building-material applications. Its product range includes jaw plates, cone crusher mantles and bowl liners, and crusher hammers.
Drawings or physical samples can be used to assess a replacement part. Provide the machine model, feed characteristics and previous wear pattern so that material and fit can be reviewed together.
Keep the feed distribution as even as the machine design allows and follow the equipment instructions for handling tramp metal. Inspect plate wear, cracks and fastening condition at the recommended intervals.
Reverse or exchange a plate only where the equipment design and maintenance procedure permit it. Base replacement decisions on the remaining profile, minimum allowable thickness, product size and inspection findings rather than on a universal service-life promise.
For equipment fit, material selection and custom casting enquiries, see our wear parts FAQ or contact Red Apple Casting.
A bimetallic crusher hammer combines a wear-resistant working head with a tougher shank. Review material choices, bonding quality and the details needed for custom manufacture.
A bimetallic hammer is designed to combine a wear-resistant working section with a tougher mounting section. The head contacts the feed, while the shank and pin-bore region support the hammer and transmit loads to the rotor.
The objective is a practical balance of abrasion resistance, impact resistance and structural integrity. Neither section should be specified solely on the basis of a maximum hardness value.
High chromium cast iron is one material option for the working section. Its carbide-containing structure can resist abrasive wear, provided that the alloy and heat treatment are suitable for the application.
Chromium content, carbon content and the required hardness depend on the specified grade and process. The suitability of a high chromium head also depends on feed size, impact severity and the risk of tramp metal; it should not be assumed to suit every hard-rock duty.
The mounting section needs sufficient strength and toughness around the pin bore and other loaded areas. Medium-carbon low-alloy steel is one possible choice, with the grade and heat treatment confirmed for the design loads.
Dimensions, bore tolerance, section transitions, mass and operating speed are important inputs. A tough shank reduces one source of risk, but it does not eliminate the need to check the complete hammer design and operating conditions.
Composite casting may use controlled pouring of two molten metals or casting a wear-resistant section around a prepared support. The process must control the interface between the two materials.
The presence of a metallurgical bond should be supported by appropriate process control and agreed inspection or qualification records. Do not assume that every composite interface is stronger than every alternative joint, or that the interface can never fail.
Red Apple Casting can review drawings, samples or pattern information for a custom hammer. Provide the crusher model, hammer dimensions, pin bore, single-piece mass, material being processed, feed size and any history of cracking or uneven wear.
Agree the material grades, heat treatment, interface requirements and acceptance criteria before manufacture. Actual service life should be assessed from operating records for comparable duty.
For equipment fit, material selection and custom casting enquiries, see our wear parts FAQ or contact Red Apple Casting.
Non-destructive testing for custom cast iron fittings should match the material, geometry, service duty and agreed acceptance requirements. Learn what to specify before ordering.
Custom cast iron fittings may require non-destructive testing, particularly where defects could affect pressure containment, load carrying or the reliability of a critical process. The required method and coverage must be determined for the actual component.
There is no single test that is automatically mandatory or technically suitable for every non-standard fitting. Applicable product requirements, the approved drawing, service conditions and the purchase agreement should define the inspection plan.
A new geometry, section thickness or casting arrangement can create different manufacturing challenges from an established standard part. Inspection should therefore address the areas that matter to the component function.
Visual and dimensional checks, material verification and selected non-destructive methods provide different information. No individual check guarantees that a casting is free of every possible defect.
Ultrasonic testing may be used to investigate internal discontinuities where the material structure, wall thickness, shape and surface condition allow a reliable examination. Cast iron can present acoustic limitations, so the test procedure and reference conditions need careful selection.
Magnetic particle testing applies to ferromagnetic materials and is primarily used for surface and near-surface discontinuities. Liquid penetrant testing is used to reveal surface-breaking discontinuities on suitable surfaces. Neither method should be described as a universal substitute for internal inspection.
Other methods may be appropriate for a particular specification, but they should be agreed on their technical merits. A standard number should not be cited as a blanket obligation without checking its actual scope.
Provide the drawing, material grade, critical dimensions, intended service, operating conditions and any specified acceptance standard. Agree which areas are examined, the method, the acceptance level and the report format.
Red Apple Casting can discuss the inspection requirements associated with a custom casting enquiry. The inspection scope for a particular order should be documented rather than inferred from a general statement that all castings are tested in the same way.
For equipment fit, material selection and custom casting enquiries, see our wear parts FAQ or contact Red Apple Casting.
Match a slurry pump casing and impeller by hydraulic duty, part geometry, clearances and material compatibility. A shared pump size alone does not confirm interchangeability.
The impeller transfers energy to the slurry, and the casing or volute guides the flow and contributes to pressure recovery. Their geometry and working clearances must be compatible with the complete pump design.
A mismatched pair can increase hydraulic losses, vibration and local wear. Parts that appear similar, or that share a nominal pump size, are not necessarily interchangeable.
Identify the required flow rate and head, the pump speed and the system characteristics. Also record slurry density, solids concentration, particle size distribution, temperature and chemistry.
The proposed pump configuration should operate within the range recommended for that pump. Operation far from the intended duty can affect efficiency and wear, so a part replacement should not be used to mask a system-selection problem.
Confirm the casing version, impeller diameter, vane arrangement, rotation, shaft connection and the relevant part numbers. Check the specified clearances and the relationship to the liners, throat bush and sealing arrangement.
Closed, open or other impeller arrangements are design choices for particular duties. An impeller type should not be selected solely because it is generally described as efficient. Back vanes and other features must also match the approved design.
High chromium white iron is used in some abrasive slurry applications, while other metallic or non-metallic systems suit different conditions. The casing and impeller materials need to be compatible with the design and duty; they do not always have to be identical.
Consider the wear and corrosion mechanisms acting on each part. Confirm the specified grades, heat treatment, dimensions and inspection requirements for any replacement casting.
Provide the pump model, casing and impeller part numbers, drawings, material specifications, operating point and wear photographs. Record whether the issue is rapid wear, vibration, reduced head, leakage or repeated failure.
Red Apple Casting can review a custom casting enquiry against the supplied technical information. Final hydraulic suitability and the installation requirements should be confirmed against the pump design and the responsible equipment supplier.
For equipment fit, material selection and custom casting enquiries, see our wear parts FAQ or contact Red Apple Casting.


The price is twice that of the small sand stone production line, and the wear-resistant hammer has strong economic benefits.
Compared with ordinary high manganese steel hammers, it has high hardness and high wear resistance. Really good.

 CN
The low price and good economic efficiency are not easy to break. The service life of the high chromium alloy hammer is 4 times that of forged or high manganese steel.